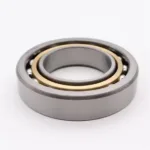
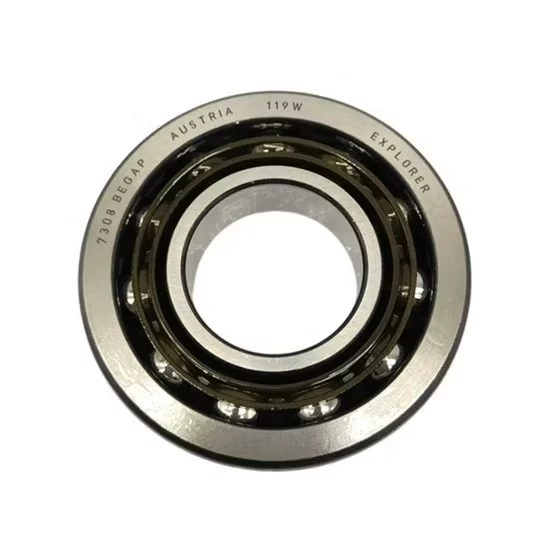
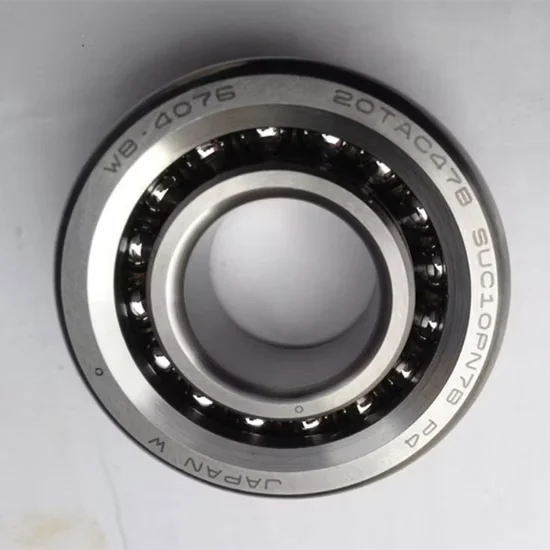
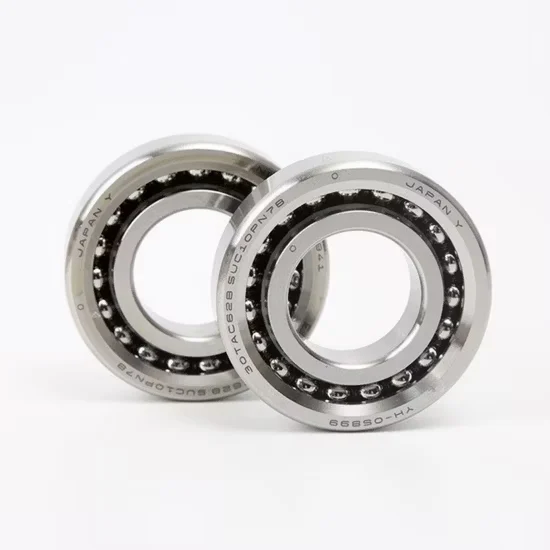
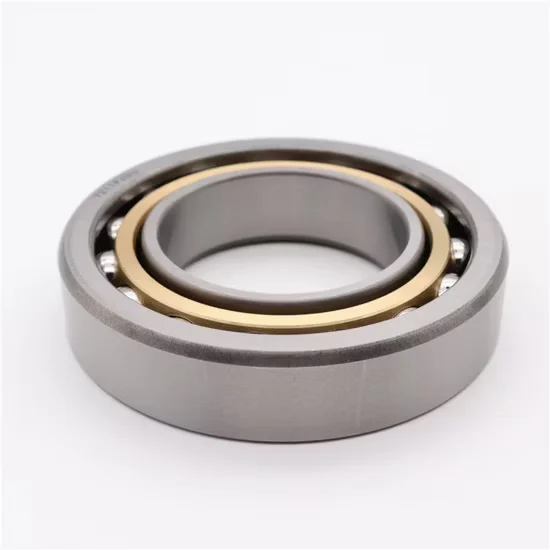
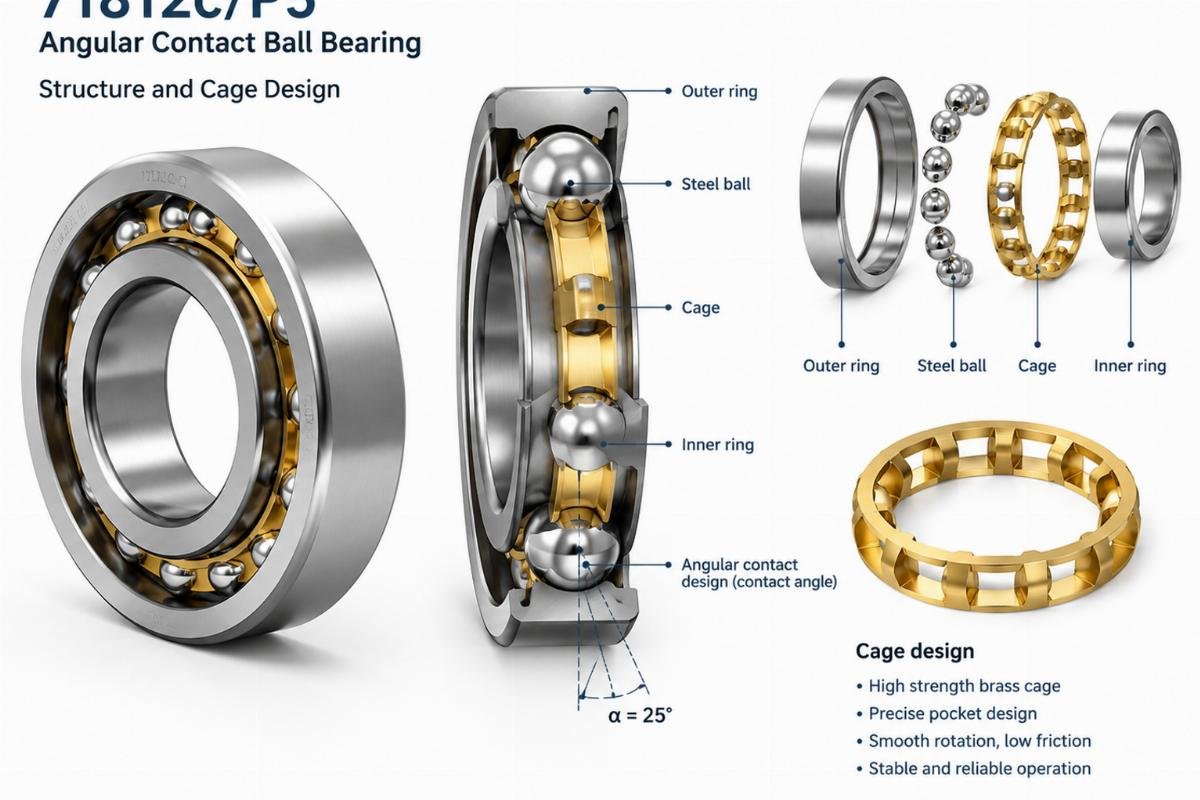
71812c/P5 Angular Contact Ball Bearing features a 15° contact angle to optimize load distribution and P5 precision class for accurate CNC spindle rotation.
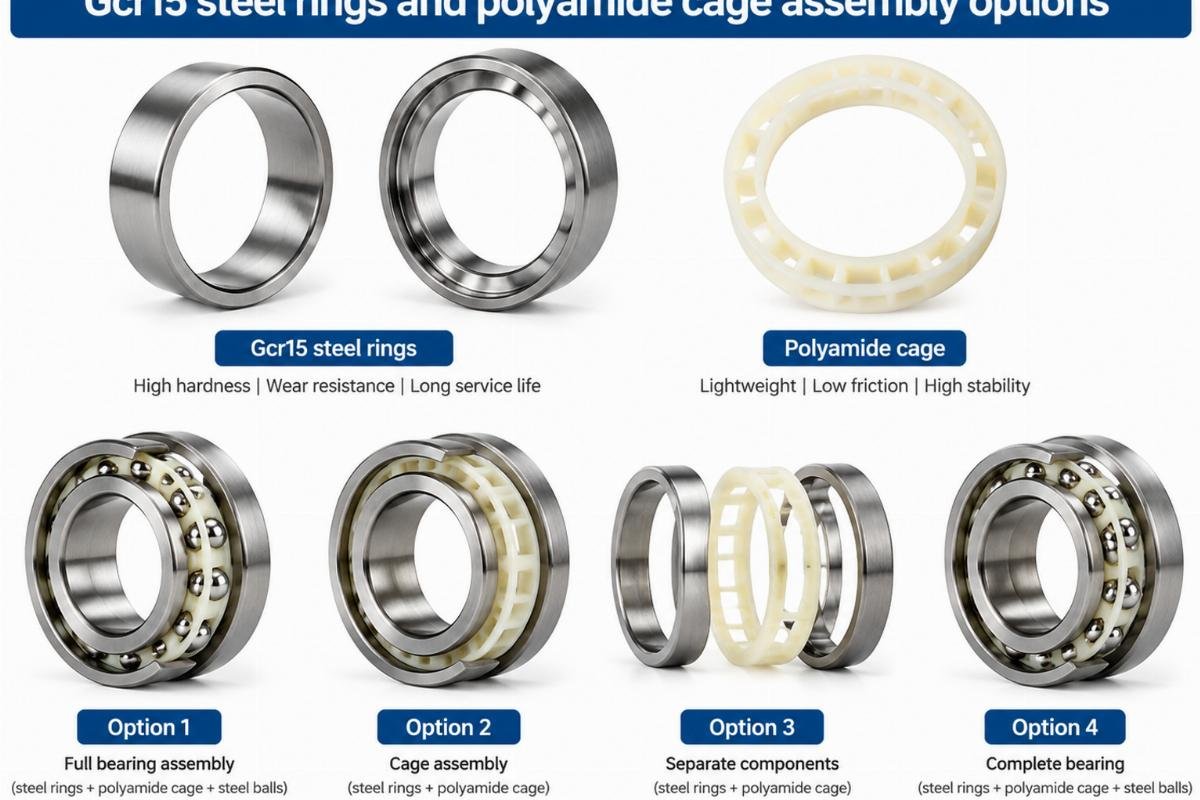
Manufactured from premium Gcr15 bearing steel, it provides high rigidity and low vibration during continuous high speed machining operations.
Always verify product authenticity by scanning the QR code through the official app channel upon receipt.
Original Batch Traceability — Every 71812c/P5 angular contact ball bearing ships with verifiable factory lot documentation to guarantee P5 precision authenticity.
Technical Specifications
Parameter
Value
Designation
71812c/P5
Bearing Type
Angular Contact Ball Bearing
Contact Angle
15° (c suffix)
Precision Class
P5
Cage Material
Nylon (Polyamide)
Material
Gcr15 Bearing Steel
Seal or Shield Type
Open
Clearance Class
C0, C1, C2, C3, C4, C5 (available options)
Vibration Level
V1, V2, V3
Rows Number
Single Row
Origin
Shandong, China
Application Suitability
Industry
Typical Applications
Machine Tool Manufacturing
CNC Spindles, High-Speed Machining Centers
Fluid Machinery
High-Speed Pumps, Industrial Compressors
Precision Engineering
High-Speed Machine Tools, Grinding Spindles
Why Spindle Vibration Spikes When a Faulty 71812c/P5 angular contact ball bearing Is Installed
Precision loss starts the moment a standard-grade replacement enters a high-speed machining center.
When a CNC spindle operates at extreme RPMs, microscopic dimensional deviations translate directly into severe surface finish defects and unacceptable tool wear. I once saw an entire production line in West Africa halt because a shipment of precision bearings was accidentally dispatched as standard tolerance due to a documentation oversight. The resulting vibration exceeded acceptable thresholds immediately upon startup, ruining expensive workpieces. Securing the correct 71812c/P5 angular contact ball bearing ensures the dimensional and running accuracy required to prevent such catastrophic unplanned downtime and maintain tight machining tolerances [NEED_CITE: rolling bearing failure mode classification per ISO 15243].
Matching High-Speed Demands with Precision Engineering
High-speed machining centers demand components that maintain rigidity under combined radial and axial loads. The 71812c/P5 angular contact ball bearing delivers this stability through its optimized 15° contact angle, which effectively balances load distribution while minimizing friction heat generation. Our engineering team verifies these specific tolerance grades before dispatch, ensuring they meet the strict rotational accuracy requirements of modern CNC spindles.
Managing Thermal Expansion and Lubrication Constraints
Spindle environments generate significant thermal gradients that directly impact internal clearance and lubrication film thickness. As operating temperatures rise, standard clearance bearings may experience excessive preload, leading to premature failure and increased friction. Selecting the appropriate clearance class from C0 to C5 is critical to accommodate these thermal expansions and maintain optimal rolling conditions. Furthermore, open-type designs require careful external lubrication management, often utilizing oil-air or oil-mist systems to maintain adequate film thickness without introducing excessive fluid friction at high rotational speeds. Ignoring these thermal and tribological factors will inevitably compromise the operational lifespan of the assembly [NEED_CITE: thermal effects on bearing internal clearance].
Decoding the Polyamide Cage and P5 Tolerance
The integration of a nylon polyamide cage significantly reduces the overall weight of the rotating assembly, which in turn lowers centrifugal forces acting on the rolling elements. This lightweight construction is essential for maintaining low vibration levels (V1, V2, or V3) during high-speed operation, directly improving the surface finish of machined parts. Additionally, the P5 precision class dictates stringent manufacturing tolerances for both bore and outside diameter, guaranteeing the exact fitment needed for precision spindle housings. The Gcr15 bearing steel provides the necessary contact fatigue strength to withstand continuous cyclic loading, ensuring a reliable operational lifespan under demanding machining conditions.
The Financial Impact of Tolerance Mismatches
Installing a bearing with incorrect precision or contact angle specifications inevitably leads to accelerated wear and compromised machining accuracy. According to ISO 281 frameworks, inadequate internal clearance or mismatched contact angles drastically reduce the calculated rating life under combined loading conditions. This premature degradation not only necessitates frequent spindle teardowns but also results in scrapped workpieces, increased tool consumption, and voided equipment warranties. The hidden costs of such unplanned downtime far exceed the initial procurement savings of substituting a lower-grade component, making strict adherence to specified tolerances a financial imperative for any manufacturing facility [NEED_CITE: economic impact of unplanned machine tool downtime].
Securing Authentic Precision Components
Sourcing genuine precision bearings requires rigorous verification beyond standard catalog matching. We specifically audit the P5 tolerance certificates and 15° contact angle verification reports for every batch, preventing the common pitfall of receiving standard-grade substitutes. Our inventory covers a comprehensive range of clearance options, allowing us to fulfill urgent maintenance requirements without compromising on exact specifications. Furthermore, we provide cross-reference consultation to ensure equivalent models from other premium brands maintain identical precision and cage material characteristics when direct replacements are unavailable.
Documentation & Authenticity
Certificate of Conformity explicitly stating P5 precision class and 15° contact angle.
Original factory batch traceability documents linking the specific lot to production records.
Dimensional and running accuracy inspection reports verifying tight P5 tolerances before dispatch.
Material test certificates confirming Gcr15 bearing steel composition and heat treatment standards.
Vibration level test data validating smooth operation for high-speed spindle applications.
Storage, Handling & Mounting
Store the open-type bearing in its original moisture-proof packaging until the exact moment of spindle assembly.
Use clean, lint-free gloves during handling to prevent microscopic contaminants from compromising the P5 running accuracy.
Apply the specified spindle oil immediately after unsealing to protect the Gcr15 steel surfaces from corrosion.
Verify the shaft shoulder runout before mounting to ensure the 15° contact angle loads evenly across rolling elements.
Maintain strict temperature control in the storage area to prevent thermal shock that could alter the precise internal clearance.
Technical Review and Selection Guidance
To ensure optimal spindle performance, please provide your specific radial and axial load profiles, maximum operating speeds, and anticipated thermal gradients. Sharing the original equipment manufacturer part numbers allows our technical team to perform precise cross-reference validation and confirm the correct clearance class. This detailed operating condition data enables us to recommend the most suitable vibration level and verify the L10 rating life for your exact machining application.
Frequently Asked Questions
Q: What do the “c” and “P5” suffixes specifically indicate for this component?
A: The lowercase “c” designates a 15° contact angle, optimizing the balance between radial and axial load capacity for high-speed spindles. The “P5” suffix denotes a high-precision tolerance class, ensuring strict dimensional and running accuracy. This combination is critical for minimizing vibration and maintaining surface finish quality in CNC machining centers.
Q: How should I select the correct internal clearance for a high-speed spindle?
A: Internal clearance selection depends on the operating temperature gradient and the required spindle rigidity. Higher speeds generate more heat, causing the inner ring to expand more than the outer ring, which reduces internal clearance. Engineers typically select a specific clearance class, such as C1 or C2, to ensure a slight preload is achieved at operating temperature, preventing skidding while avoiding excessive friction.
Q: What are the selection boundaries between polyamide and brass cages in machine tools?
A: Polyamide cages are significantly lighter, reducing centrifugal forces and allowing for higher speed limits, making them ideal for most high-speed CNC spindles. Brass cages offer superior durability under heavy loads, high temperatures, or aggressive lubrication conditions where polymer degradation might occur. The choice ultimately depends on the maximum operating speed and the specific lubrication method used in the spindle design.
Q: How can I verify the authenticity of the received precision bearings?
A: Authenticity verification requires checking the factory batch traceability documents and matching them with the physical markings on the bearing rings. You should also request the original dimensional and running accuracy inspection reports to confirm the P5 tolerances. Additionally, verifying the material certificates ensures the rings are manufactured from genuine Gcr15 bearing steel with proper heat treatment.
Q: Why is spindle vibration exceeding acceptable limits after replacing the bearings?
A: Excessive vibration often stems from installing a bearing with an incorrect precision class, mismatched contact angle, or improper internal clearance. If a standard-tolerance bearing is used instead of a P5 grade, the dimensional deviations will cause severe runout. Furthermore, failing to account for thermal expansion during clearance selection can lead to excessive preload, generating heat and amplifying vibration during high-speed operation.
Shipping Information
EU Warehouse
3-7 working days (bonded stock)
Direct from China
Shanghai & Ningbo hubs (bulk / FCL)
Markets Served
DE · IT · PL · ES · NL · FR · EU+
Incoterms
DDP / DAP available on request
Minimum Order
Contact us for MOQ details
Documents Included with Every Shipment
EN and ISO Quality Certificates
Batch traceability and manufacturing standard
Material & Heat-Treatment Reports
Full material composition and process records
CE Declaration of Conformity
For bearing units and motion products
RoHS Compliance Declaration
Restriction of hazardous substances
EUR.1 Movement Certificate
Preferential origin for EU customs
Certificate of Origin
Country of manufacture documentation
Correct HS Codes
Pre-classified for smooth customs clearance
Commercial Invoice & Packing List
VAT-compliant intra-EU invoicing
Transparent Landed Cost with Tax Explanation
SKFEU provides full price transparency so EU buyers know exactly what they pay. No hidden duties, no surprise charges at customs.
VAT-Compliant Invoicing
All intra-EU transactions are invoiced with correct VAT treatment. B2B buyers with valid EU VAT numbers receive zero-rated invoices where applicable.
No Unexpected Import Duties
Goods shipped from our EU bonded warehouse arrive as intra-EU movements -- no import duties, no customs delays for EU-based buyers.
EUR.1 & Origin Docs Ready
For shipments direct from China, EUR.1 movement certificates and certificates of origin are prepared in advance to minimise customs clearance time.
DDP Pricing Available
Ask for Delivered Duty Paid quotations -- we absorb all import costs so your landed cost is fixed and predictable from day one.
Need a landed cost breakdown? Contact Sofia at
sofia@skfeu.com
or via WhatsApp for a full DDP quotation including freight, duties and VAT for your country.
Send Inquiry
Request Pricing & Availability
Share your requirements and Sofia will respond within one working day with pricing, lead time and full documentation details.