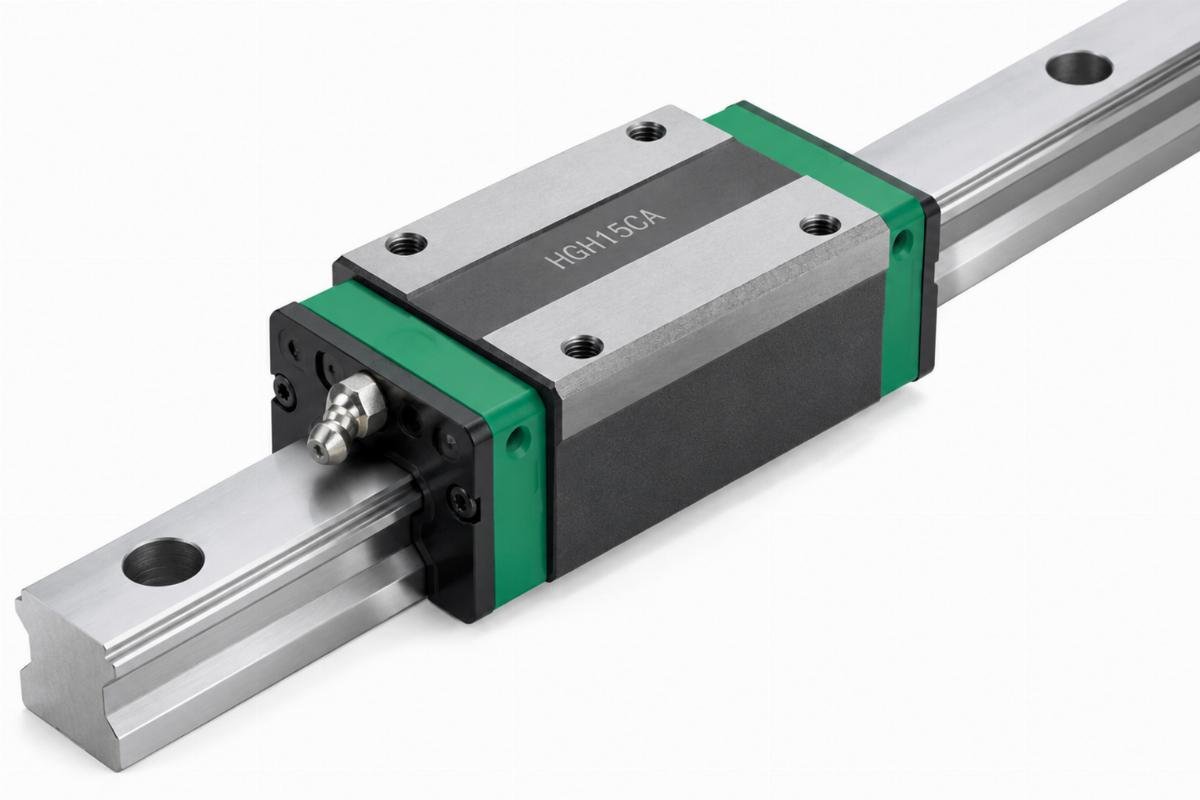
HGH15ca Linear Guide Rail Steel with Carriage Sliding Block Kits for CNC Machine
HGH15ca Linear Guide Rail provides precise motion transmission for industrial CNC machines, featuring Gcr15 bearing steel construction and galvanized surface treatment for high corrosion resistance.
The solid profile structure ensures low noise operation and very smooth sliding performance.
Every shipment includes a complete documentation package with material certificates and dimensional inspection reports to guarantee verified quality.
Cross-Reference Alignment Verified — We validate dimensional interchangeability across EGH and MGN series before dispatching any HGH15ca linear guide rail shipment.
Technical Specifications
Parameter
Value
Designation
HGH15ca
Material
Gcr15 bearing steel
Surface Treatment
Galvanized
Profile Type
Solid profile
Support Rail Length
100-4000mm custom lengths
Corrosion Resistance
High corrosion resistance
Performance
Low noise, very smooth operation
Certification
CE, EPA, ISO 9001:2000, RoHS
Origin
Shandong, China
Note: The “ca” designation is an unverified suffix requiring manufacturer catalog confirmation to ascertain its exact preload or flange configuration.
Application Suitability
Industry
Typical Applications
Machine Tools
CNC machine spindle traverse axes
Linear Motion
Automated assembly line transfer carriages
General Manufacturing
Precision grinding machine worktable guides
Why Ignoring Preload Suffixes Wrecks Your HGH15ca linear guide rail Setup
Mismatched preload classes cause high-speed vibration that no amount of realignment can fix.
I learned this the hard way in Vietnam when a CNC retrofit suffered severe chatter during high-speed machining. We only checked basic dimensions and missed the preload specification. Swapping to a heavy preload carriage stabilized the system, proving that assuming standard clearance works for every HGH15ca linear guide rail application is a costly mistake. The dynamic forces in milling operations demand exact rigidity. When the internal ball bearing arrangement lacks the correct preload, the carriage block experiences micro-displacements under cutting loads. This not only degrades surface finish quality but also accelerates fatigue on the raceways. [NEED_CITE: linear guideway preload selection guidelines for machine tools]
Matching Solid Profile Rails to Precision Machining Demands
When outfitting CNC equipment, the solid profile construction of this HGH15ca linear guide rail provides the rigidity needed for heavy cutting loads. Our sourcing network ensures you receive components that maintain strict geometric tolerances under continuous operation. By cross-referencing equivalent models like HGW or MGN, we help procurement teams secure compatible replacements without compromising the original machine design. The structural integrity of the solid profile prevents deflection during aggressive material removal, ensuring the tool tip remains precisely on target.
Navigating Contamination and Load Reversals in Automation
Machine tool environments expose linear motion components to metallic dust and coolant splashes, demanding high corrosion resistance and effective sealing. The galvanized surface treatment on these rails offers a strong defense against moisture, while the carriage block design must handle combined radial and reverse axial loads during rapid traverse. Proper lubrication intervals are critical to prevent particulate ingress from accelerating wear. Coolant fluids often contain corrosive additives that can degrade unprotected steel surfaces over time. By specifying high corrosion resistance materials and treatments, maintenance teams can significantly reduce the frequency of unplanned carriage block replacements. [NEED_CITE: linear motion system contamination and lubrication practices]
Decoding Material Traits and Interchangeability
The Gcr15 bearing steel material delivers excellent rolling contact fatigue resistance, making it suitable for demanding linear motion transmission equipment. When substituting with EGH or EGW variants, engineers must carefully align the internal carriage ball recirculation design to avoid binding. The high carbon chromium composition of Gcr15 ensures that the raceways can withstand millions of stress cycles without spalling. Understanding these metallurgical traits helps buyers evaluate whether the selected components will survive the rigorous demands of continuous multi-axis machining.
The Hidden Toll of Incorrect Carriage Block Substitution
Forcing an incompatible carriage block onto a precision rail leads to premature failure and catastrophic damage to the machined workpiece. According to failure analysis frameworks similar to ISO 15243, improper preload or mismatched ball sizes generate excessive internal friction and heat. This results in unplanned downtime and warranty voidance, turning a minor component swap into a major production bottleneck. Avoiding these hidden costs requires rigorous technical validation before any physical installation takes place on the shop floor. [NEED_CITE: linear guideway failure modes and root cause analysis]
Securing Traceable Linear Motion Components
Sourcing mixed-brand packages often leads to mismatched tolerances, but we provide complete traceability documentation for every HGH15ca linear guide rail kit. Our technical team conducts cross-brand equivalent model consultations to ensure the carriage block and rail profiles align perfectly. We maintain massive spot inventory covering thousands of standard part numbers, allowing flexible MOQ from single-unit emergency spares to full container consolidation. Furthermore, our global shipping consolidation and long-term after-sales technical support guarantee that your CNC machines stay operational. We understand that a missing carriage block can halt an entire production line, which is why our logistics network prioritizes rapid dispatch for critical maintenance requirements.
Documentation & Authenticity
Material test reports confirming Gcr15 steel composition for the solid profile rails.
Dimensional inspection certificates verifying straightness across custom 100-4000mm lengths.
Certificate of Conformity aligning with ISO 9001:2000 and RoHS standards.
Origin documents detailing the Shandong manufacturing facility for customs clearance.
Storage, Handling & Mounting
Store the galvanized rails in original packaging to prevent moisture from compromising high corrosion resistance.
Use clean gloves when handling carriage blocks to avoid transferring skin oils to Gcr15 steel surfaces.
Keep matched rail and block sets sealed until mounting to preserve factory alignment and low noise performance.
Apply recommended grease to carriage block recirculation caps before installing on custom length support rails.
Preparing Your Technical Parameters for Selection
To ensure optimal performance, please share your specific radial and axial load profiles, operating speeds, and environmental conditions. If you are replacing an existing system, providing the OEM equipment number or detailed carriage block dimensions allows our engineering team to perform an accurate cross-reference check. This technical review guarantees the selected linear motion components meet your exact CNC machining requirements. Detailing the expected duty cycle and ambient temperature fluctuations also helps us recommend the most appropriate lubrication strategy and sealing configuration for your specific application.
Frequently Asked Questions
Q: What does the suffix on this model indicate regarding preload?
A: The specific suffix on this model remains unverified in standard public catalogs, so we strongly recommend checking your original equipment manufacturer’s manual. Our technical support team can also assist by comparing your existing carriage block dimensions against our internal cross-reference database to ensure a perfect match.
Q: Can I substitute this model with EGH or MGN series equivalents?
A: While EGH, EGW, HGH, HGW, MGN, and MGW series share similar dimensional envelopes, internal carriage designs and ball recirculation paths often differ. Substituting without verifying the exact preload class and flange mounting hole patterns can cause binding. Always consult our engineering team for a detailed interchangeability analysis before ordering.
Q: How does the galvanized treatment affect lifespan in harsh environments?
A: The galvanized surface treatment provides high corrosion resistance against coolant splashes and humid workshop conditions. This protective layer significantly extends the service life of the Gcr15 steel rails compared to untreated alternatives, ensuring very smooth operation and preventing surface pitting that could otherwise disrupt the carriage block’s linear motion.
Q: What is the best way to ensure straightness for custom 4000mm rails?
A: For support rail lengths approaching 4000mm, maintaining dimensional accuracy requires specialized handling and precise mounting techniques. We recommend using multiple alignment pins and checking straightness with a dial indicator during installation. Our dimensional inspection reports confirm the initial straightness tolerance before the rails are shipped from our facility.
Q: What lubrication practices are recommended for heavy-duty CNC applications?
A: Heavy-duty CNC machining generates significant heat and particulate contamination, demanding regular relubrication. Use a high-quality lithium-based grease applied directly to the carriage block grease nipples. Establish a maintenance schedule based on your machine’s operating hours to flush out metallic debris and maintain the low noise, very smooth performance of the linear guide system.
Shipping Information
EU Warehouse
3-7 working days (bonded stock)
Direct from China
Shanghai & Ningbo hubs (bulk / FCL)
Markets Served
DE · IT · PL · ES · NL · FR · EU+
Incoterms
DDP / DAP available on request
Minimum Order
Contact us for MOQ details
Documents Included with Every Shipment
EN and ISO Quality Certificates
Batch traceability and manufacturing standard
Material & Heat-Treatment Reports
Full material composition and process records
CE Declaration of Conformity
For bearing units and motion products
RoHS Compliance Declaration
Restriction of hazardous substances
EUR.1 Movement Certificate
Preferential origin for EU customs
Certificate of Origin
Country of manufacture documentation
Correct HS Codes
Pre-classified for smooth customs clearance
Commercial Invoice & Packing List
VAT-compliant intra-EU invoicing
Transparent Landed Cost with Tax Explanation
SKFEU provides full price transparency so EU buyers know exactly what they pay. No hidden duties, no surprise charges at customs.
VAT-Compliant Invoicing
All intra-EU transactions are invoiced with correct VAT treatment. B2B buyers with valid EU VAT numbers receive zero-rated invoices where applicable.
No Unexpected Import Duties
Goods shipped from our EU bonded warehouse arrive as intra-EU movements -- no import duties, no customs delays for EU-based buyers.
EUR.1 & Origin Docs Ready
For shipments direct from China, EUR.1 movement certificates and certificates of origin are prepared in advance to minimise customs clearance time.
DDP Pricing Available
Ask for Delivered Duty Paid quotations -- we absorb all import costs so your landed cost is fixed and predictable from day one.
Need a landed cost breakdown? Contact Sofia at
sofia@skfeu.com
or via WhatsApp for a full DDP quotation including freight, duties and VAT for your country.
Send Inquiry
Request Pricing & Availability
Share your requirements and Sofia will respond within one working day with pricing, lead time and full documentation details.