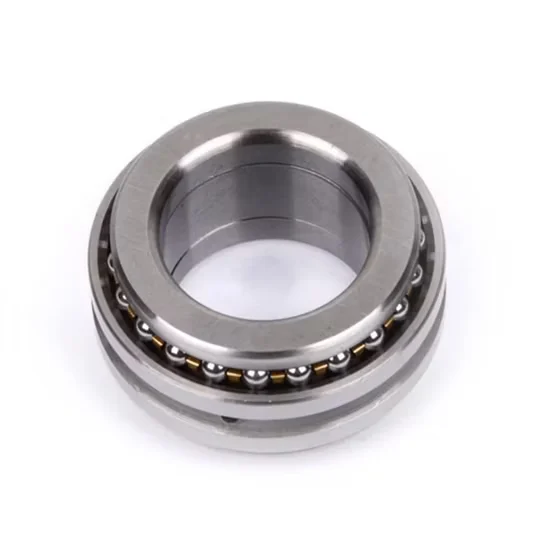
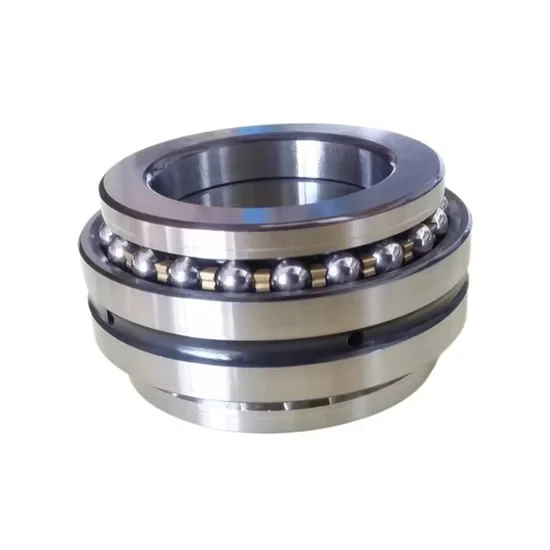
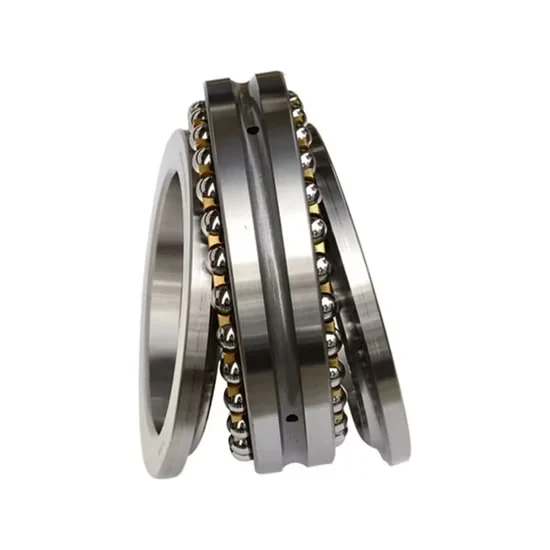
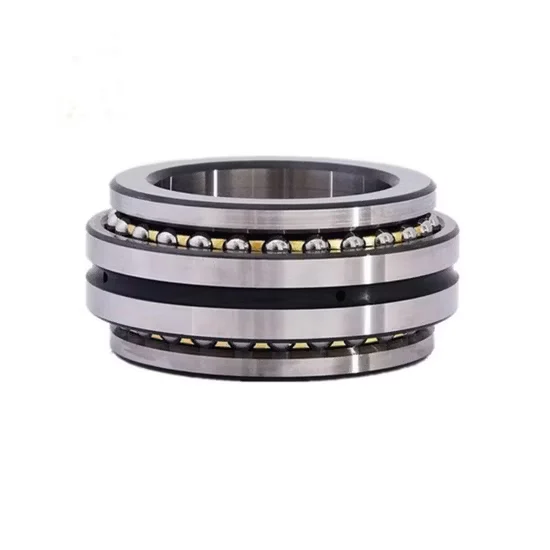
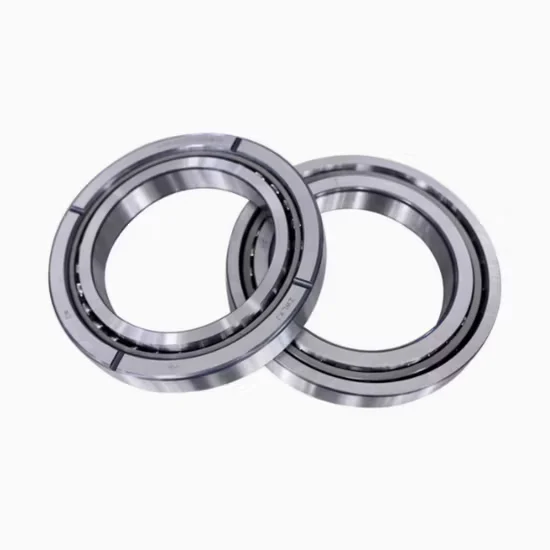
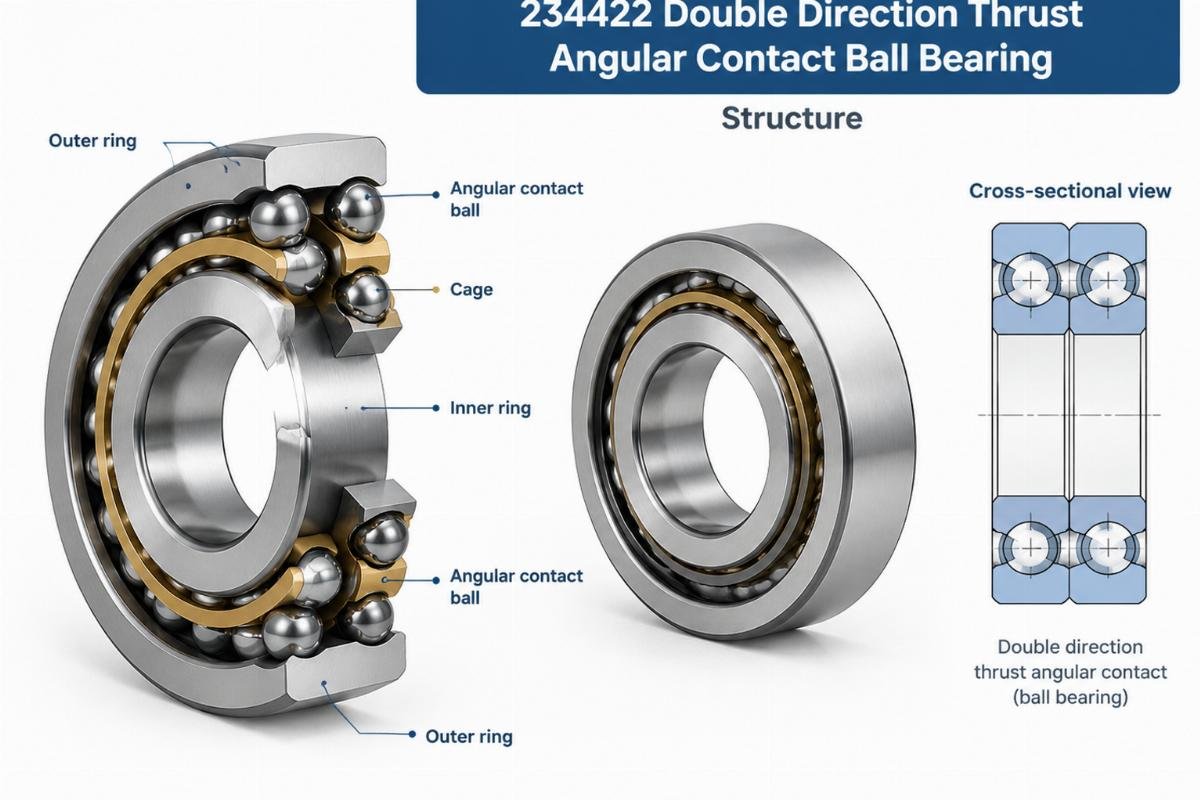
234422 Double Direction Thrust Angular Contact Ball Bearing P4/P2 — featuring Gcr15 bearing steel and an open seal design optimized for machine tool spindles and precision equipment.
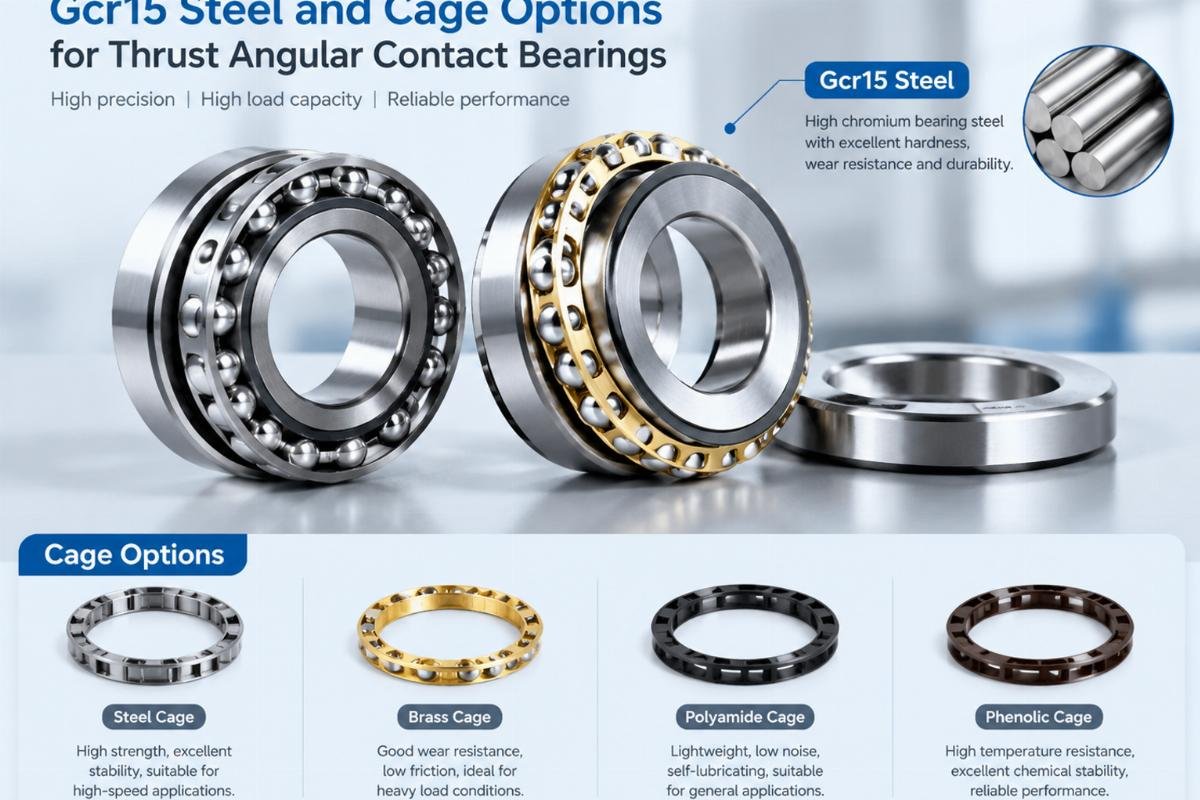
The unseparated structure with brass, nylon, or steel cages ensures high axial rigidity under double direction thrust loads.
Always verify cross reference alignment for cage material, precision class, and exact dimensional specs before final procurement.
Official QR Verification — Every 234422 double direction thrust angular contact ball bearing ships with scannable traceability tags linking directly to the manufacturer’s authentication database.
Technical Specifications
Parameter
Value
Designation
234422
Bearing Type
Double Direction Thrust Angular Contact Ball Bearing
Material
Gcr15 (Suj2) Bearing Steel
Cage Material
Brass, Nylon, or Steel options
Seal or Shield Type
Open
Precision Class
P0, P6, P5, P4, P2
Arrangement
Unseparated
Origin
Shandong, China
Application Suitability
Industry
Typical Applications
Machine Tool Manufacturing
Vertical and horizontal spindle assemblies requiring high axial rigidity
Precision Equipment
High-speed rotary tables and indexing heads
Robotics
Articulation joints demanding precise axial positioning and load support
Why Spindle Vibration Often Traces Back to the 234422 Double Direction Thrust Angular Contact Ball Bearing Assembly
Improper thermal mounting destroys the Gcr15 steel microstructure long before the first cut is made.
I remember supplying 234420 bearings for a Brazilian machine tool plant where technicians used open-flame heating to force the fit. The localized overheating altered the metallographic structure, causing severe spindle vibration and premature scrap within months. When upgrading to the 234422 double direction thrust angular contact ball bearing, avoiding such thermal abuse is critical to maintaining the P4 or P2 running accuracy. The intense heat from improper mounting methods destroys the carefully engineered internal geometry, turning a premium component into scrap metal before the machine even starts cutting. [NEED_CITE: thermal damage to bearing rings during improper mounting]
Matching Axial Rigidity to High-Speed Spindle Demands
Machine tool spindles subject the 234422 double direction thrust angular contact ball bearing to intense bidirectional axial loads during heavy milling operations. Our sourcing network ensures you receive the exact precision class required, whether your CNC lathe needs standard P6 or ultra-precise P2 tolerances. By cross-referencing your specific spindle model, we supply matched sets that maintain axial stiffness without compromising rotational smoothness. The unseparated design inherently provides the structural rigidity necessary to absorb the thrust forces generated during aggressive facing and boring cycles, keeping the cutting tool perfectly aligned.
Managing Thermal Expansion and Lubrication in Precision Grinding
High-speed grinding generates significant friction heat, which directly impacts the internal clearance of an open-type thrust bearing. Selecting the appropriate cage material—brass for high-speed stability or steel for heavy-load resilience—helps manage these thermal gradients. Proper oil-air or oil-mist lubrication is mandatory to prevent cage wear and maintain the geometric accuracy of the rolling elements. Without a continuous supply of clean lubricant, the open design leaves the rolling contacts vulnerable to microscopic debris, accelerating fatigue and compromising the surface finish of the machined components. [NEED_CITE: lubrication methods for high-speed angular contact bearings]
Decoding Precision Classes and Cage Options for the 2344 Series
The 234422 designation indicates a specific bore and outside diameter optimized for standard machine tool housings, available in Gcr15 (Suj2) bearing steel. Since this model features an open seal design, it relies entirely on the spindle’s external lubrication system, eliminating the friction penalties associated with contact seals. The unseparated internal geometry provides the necessary axial rigidity for double-direction thrust loads, while the choice between brass, nylon, or steel cages allows engineers to balance speed limits against operational vibration. Understanding these internal variations ensures the selected configuration perfectly aligns with the thermal and mechanical realities of your specific machining environment.
The Hidden Toll of Mismatched Precision and Mounting Errors
Installing a P0 precision bearing in a high-speed CNC spindle guarantees unacceptable runout and surface finish defects on the machined parts. Beyond dimensional errors, forcing a bearing onto a shaft without controlled induction heating leads to micro-cracking in the inner ring. Such installation failures result in unplanned downtime and catastrophic damage to the spindle housing, voiding equipment warranties and escalating maintenance costs far beyond the initial component price. The resulting geometric distortion propagates through the entire machine structure, ruining batch quality and forcing complete spindle teardowns to rectify the underlying assembly mistakes. [NEED_CITE: bearing failure modes related to mounting errors per ISO 15243]
Securing Traceability and Technical Alignment for Your Spindle Rebuilds
Sourcing a genuine 234422 double direction thrust angular contact ball bearing requires more than just matching the part number; it demands verifying the exact cage material and precision class against the OEM specification. We provide complete batch traceability for KOYO, NSK, NTN, and OZD brands, ensuring no counterfeit components enter your maintenance inventory. Our technical team reviews your spindle drawings to confirm the cross-reference dimensions, preventing the costly mistake of installing an incorrect axial clearance variant. This rigorous verification process protects your production schedule from the devastating delays caused by premature bearing seizures and unexpected machine stoppages.
Documentation & Authenticity
Original factory batch traceability linking the 234422 bearing to its specific production run.
Dimensional and running accuracy inspection reports confirming P4 or P2 tolerances before dispatch.
Material certification verifying the Gcr15 (Suj2) bearing steel composition and heat treatment hardness.
Official manufacturer QR codes for instant digital authentication of KOYO, NSK, or NTN origins.
Storage, Handling & Mounting
Store the open-type 234422 bearing in its original VCI packaging to prevent moisture ingress on the Gcr15 steel surfaces.
Use controlled induction heaters for inner ring mounting; never apply open flames that destroy the P4 precision microstructure.
Keep the unseparated thrust assembly clean and covered until the exact moment of spindle integration to avoid abrasive contamination.
Apply clean, lint-free gloves when handling the brass or nylon cage variants to prevent skin acids from initiating corrosion.
Preparing Your Technical Data for Accurate Spindle Sourcing
To ensure the supplied 234422 double direction thrust angular contact ball bearing perfectly matches your equipment, please share the spindle’s operational parameters, including maximum RPM, bidirectional axial loads, and operating temperature range. Providing the original OEM equipment model number allows our engineers to cross-reference the exact precision class and cage material required. This technical review guarantees the replacement component restores your machine tool’s original machining accuracy. Supplying detailed environmental data, such as exposure to coolant mist or metallic dust, also helps us recommend the most effective external sealing arrangements for your open-type bearing setup.
Frequently Asked Questions
Q: How do I verify the authenticity of a KOYO or NSK 2344 series bearing?
A: Authenticity is confirmed by scanning the official QR code on the packaging, which links to the manufacturer’s database. We also provide original factory batch traceability documents and dimensional inspection reports. This ensures the 234422 double direction thrust angular contact ball bearing you receive is genuine and meets the specified P4 or P2 precision standards.
Q: What are the cross-reference precautions for the 234422 model?
A: When cross-referencing to equivalents like the 234421 or 234420, you must verify the exact bore diameter, precision class, and cage material. A mismatch in the internal axial clearance or cage type can cause severe spindle vibration. Always consult the OEM manual or provide the machine model number so we can validate the dimensional alignment before shipment.
Q: How should I choose between brass, nylon, and steel cages for machine tool spindles?
A: Brass cages offer excellent stability and heat dissipation for high-speed milling spindles, while steel cages provide maximum load capacity for heavy-duty cutting. Nylon cages are suitable for moderate speeds where low friction is prioritized. Selecting the right cage for your 234422 bearing depends on the specific RPM and thermal conditions of your spindle application.
Q: What is the difference between P4 and P2 precision ratings in thrust angular contact bearings?
A: P2 precision offers tighter tolerances for running accuracy and dimensional deviations compared to P4, making it essential for ultra-high-speed grinding spindles. Using a P4 bearing in a P2-designed application will result in unacceptable runout and poor surface finishes. We supply both grades with full inspection reports to match your exact machine tool requirements.
Shipping Information
EU Warehouse
3-7 working days (bonded stock)
Direct from China
Shanghai & Ningbo hubs (bulk / FCL)
Markets Served
DE · IT · PL · ES · NL · FR · EU+
Incoterms
DDP / DAP available on request
Minimum Order
Contact us for MOQ details
Documents Included with Every Shipment
EN and ISO Quality Certificates
Batch traceability and manufacturing standard
Material & Heat-Treatment Reports
Full material composition and process records
CE Declaration of Conformity
For bearing units and motion products
RoHS Compliance Declaration
Restriction of hazardous substances
EUR.1 Movement Certificate
Preferential origin for EU customs
Certificate of Origin
Country of manufacture documentation
Correct HS Codes
Pre-classified for smooth customs clearance
Commercial Invoice & Packing List
VAT-compliant intra-EU invoicing
Transparent Landed Cost with Tax Explanation
SKFEU provides full price transparency so EU buyers know exactly what they pay. No hidden duties, no surprise charges at customs.
VAT-Compliant Invoicing
All intra-EU transactions are invoiced with correct VAT treatment. B2B buyers with valid EU VAT numbers receive zero-rated invoices where applicable.
No Unexpected Import Duties
Goods shipped from our EU bonded warehouse arrive as intra-EU movements -- no import duties, no customs delays for EU-based buyers.
EUR.1 & Origin Docs Ready
For shipments direct from China, EUR.1 movement certificates and certificates of origin are prepared in advance to minimise customs clearance time.
DDP Pricing Available
Ask for Delivered Duty Paid quotations -- we absorb all import costs so your landed cost is fixed and predictable from day one.
Need a landed cost breakdown? Contact Sofia at
sofia@skfeu.com
or via WhatsApp for a full DDP quotation including freight, duties and VAT for your country.
Send Inquiry
Request Pricing & Availability
Share your requirements and Sofia will respond within one working day with pricing, lead time and full documentation details.