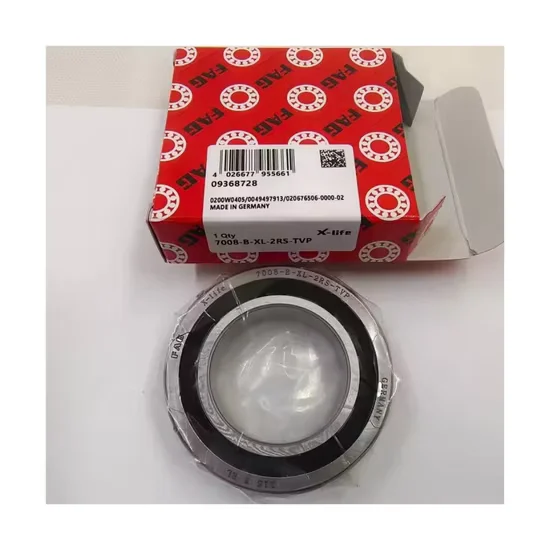
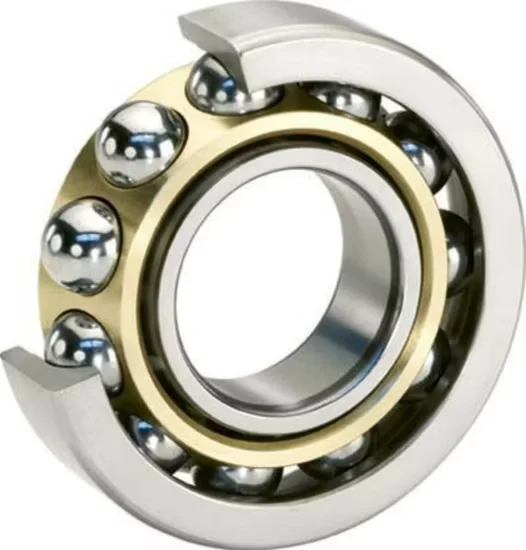
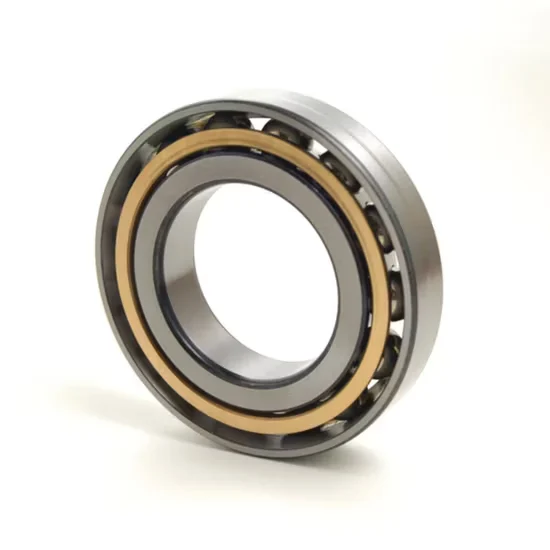
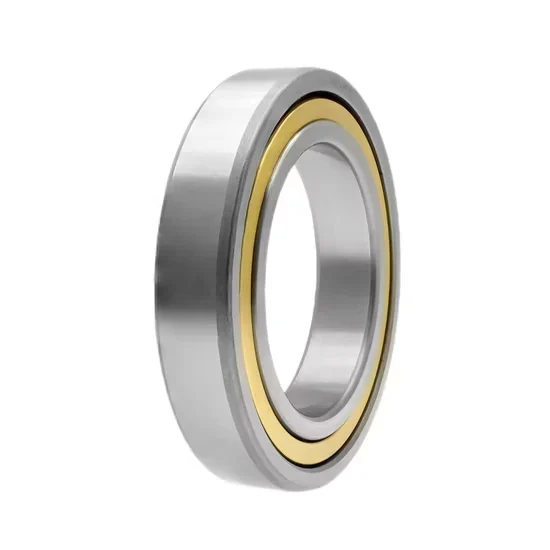
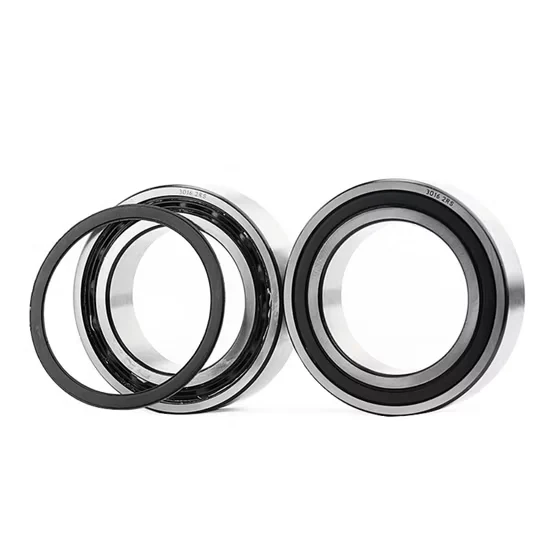
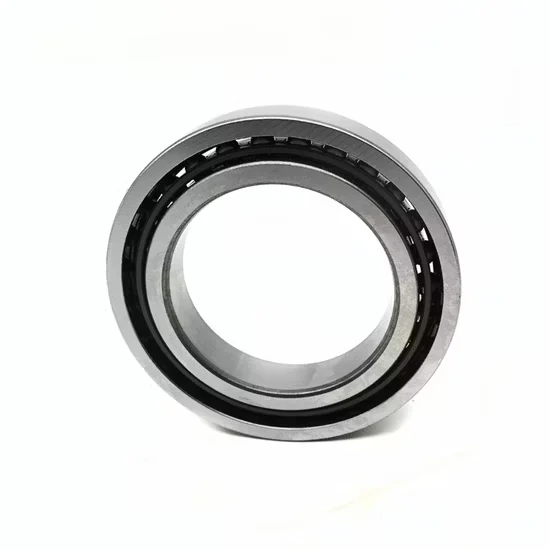
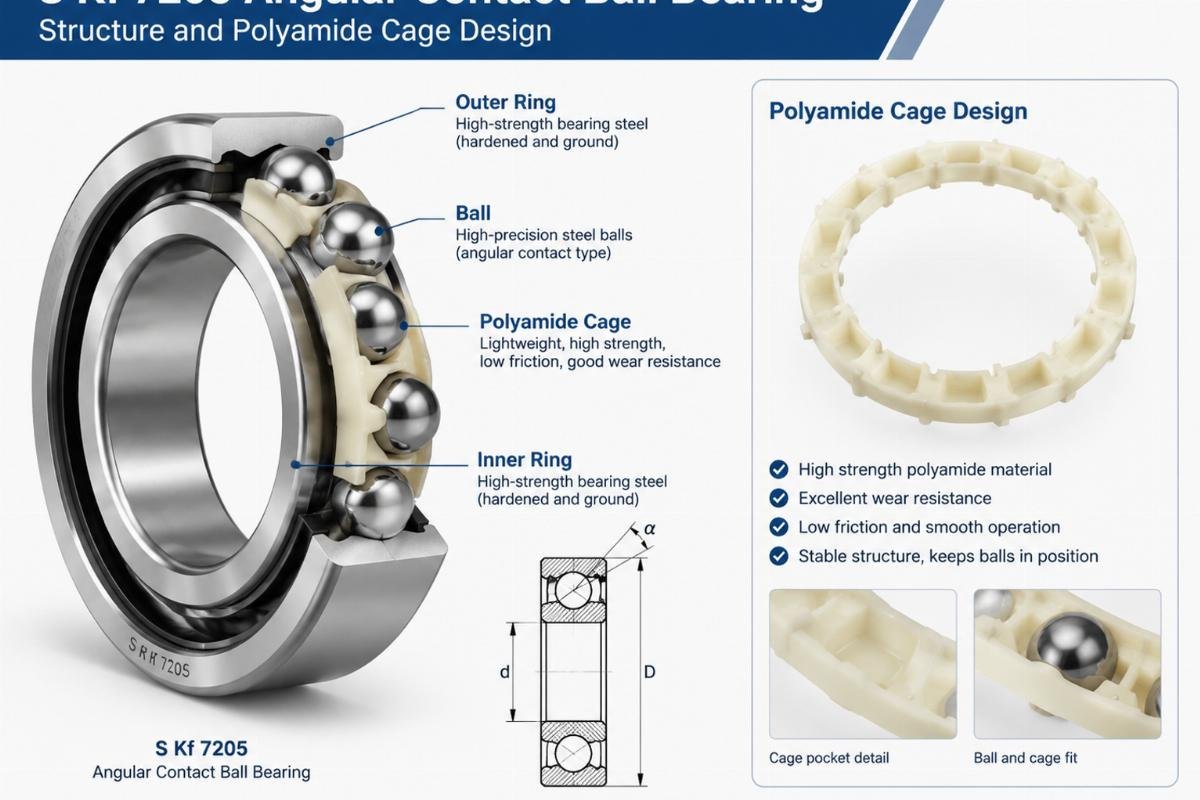
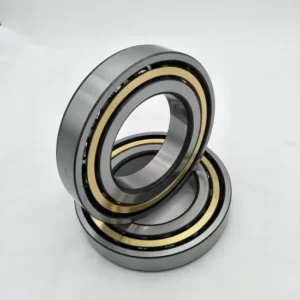
S Kf 7205 Angular Contact Ball Bearing features an open seal configuration requiring external lubrication and a polyamide cage to minimize friction during high-speed spindle applications.
Constructed with Gcr15 bearing steel for durable and reliable load capacity.
Verify product authenticity instantly by scanning the QR code through the official brand app upon delivery.
Mixed-Brand Sourcing Covered — Consolidate S Kf 7205 angular contact ball bearing orders with other premium lines in a single shipment without juggling multiple vendors.
Technical Specifications
Parameter
Value
Designation
S Kf 7205
Bearing Type
Angular Contact Ball Bearing
Contact Angle
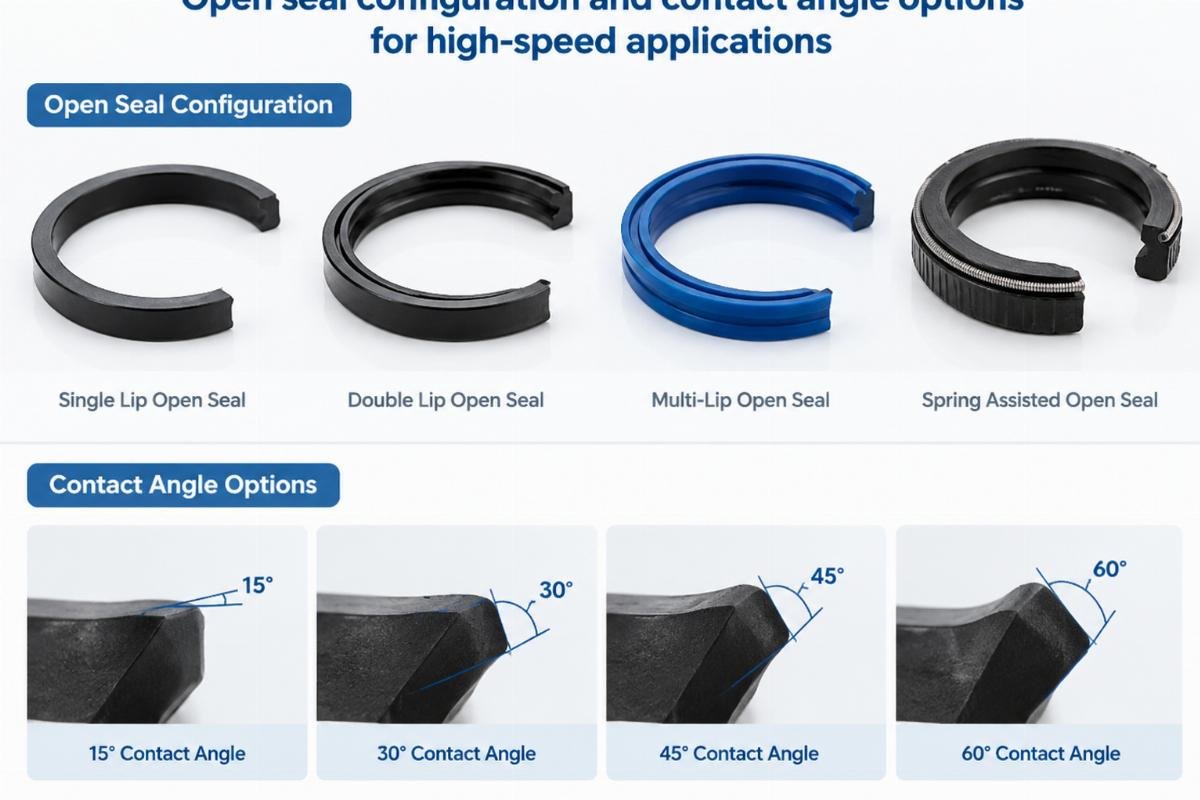
15° (C), 25° (AC), 30° (a), 40° (B)
Aligning
Non-Aligning Bearing
Separated
Unseparated
Rows Number
Single Row / Double Row
Material
Gcr15 Bearing Steel
Seal or Shield Type
Open
Cage Material
Nylon (Polyamide)
Vibration
V1, V2, V3
Clearance Class
C0, C1, C2, C3, C4, C5
Origin
Shandong, China
Application Suitability
Industry
Typical Applications
Machine Tools
High-speed spindle assemblies and precision robotic joints
Fluid Machinery
Centrifugal pump impeller supports and compressor rotors
Precision Equipment
Optical measuring instruments and automated positioning stages
Why Spindle Vibration Ruins More Than Just Surface Finish
Selecting the right S Kf 7205 angular contact ball bearing is only the first step; ignoring cage dynamics at high RPM causes catastrophic chatter.
Polyamide cages dampen high-frequency vibrations far better than stamped steel alternatives in precision spindle applications.
When a machine tool spindle starts chattering, operators often blame the cutting tool or the workpiece material. In reality, a mismatched cage material or incorrect clearance class inside the bearing generates microscopic oscillations that destroy surface finish. These sub-surface vibrations propagate through the spindle housing, accelerating tool wear and causing severe dimensional inaccuracies in the machined parts. [NEED_CITE: vibration propagation in high-speed spindle bearings]
Matching the S Kf 7205 Angular Contact Ball Bearing to Spindle Loads
High-speed spindles demand components that handle combined radial and axial loads without thermal runaway. The S Kf 7205 angular contact ball bearing accommodates these complex forces through its specific contact angle geometry, directing axial thrust efficiently into the housing. We routinely help factories cross-reference these units against existing equipment setups to ensure exact dimensional and dynamic equivalence. By analyzing the specific cutting forces and rotational speeds, our technical team ensures the selected configuration prevents premature raceway fatigue under continuous heavy milling operations.
Thermal Expansion and Lubrication Starvation in Continuous Machining
At elevated rotational speeds, friction heat rapidly alters the internal clearance of open-type bearings. If the initial clearance is too tight, thermal expansion will preload the rolling elements beyond their design limits, leading to catastrophic seizure. Proper oil-air or oil-mist lubrication is critical to carry away this heat while maintaining a stable hydrodynamic film between the rolling elements and the raceways. Without a precisely metered lubrication system, the polyamide cage can experience localized melting, completely destroying the bearing assembly within minutes of startup. [NEED_CITE: thermal displacement effects on bearing internal clearance]
Decoding Cage Materials and Contact Angle Variations
The polyamide cage significantly reduces friction and operates quietly, making it ideal for high-RPM spindle environments where brass cages might generate excess drag. Contact angles dictate the axial load capacity; a 15° angle favors pure radial and high-speed performance, while a 40° angle provides maximum thrust capacity for heavy axial cutting forces. Open seal configurations allow maintenance teams to flush the raceway and apply custom high-speed spindle oils directly, preventing the contamination buildup common in sealed variants. Clearance classes from C0 to C5 compensate for different shaft interference fits and operating temperature gradients across various machining centers. Selecting the correct vibration grade ensures the bearing meets the strict dynamic balancing requirements of precision machinery, eliminating harmonic resonance during aggressive cutting cycles.
The Cascading Failures of Incorrect Clearance Selection
Installing a standard clearance bearing in a high-speed spindle with a tight interference fit inevitably leads to premature fatigue. According to failure mode classifications per ISO 15243, this excessive internal preload causes severe raceway smearing and eventual cage fracture. The resulting unplanned downtime halts the entire production line, voiding warranties on adjacent drive motors and gearboxes. Furthermore, the sudden seizure of a spindle bearing can snap the cutting tool and damage the expensive workpiece, compounding the financial loss far beyond the cost of the replacement component. [NEED_CITE: rolling bearing failure mode classification per ISO 15243]
Securing Authentic Components for Critical Machining Operations
Counterfeit angular contact bearings often fail within weeks because their internal geometry lacks the precise grinding tolerances required for high-speed spindles. We source genuine S Kf products with complete batch traceability, ensuring the metallurgical integrity of the rings, available in Gcr15 bearing steel configurations. Our technical team verifies the exact contact angle suffix and clearance class against your spindle OEM specifications before dispatch, preventing the costly mismatch of a 40° angle where a 15° angle was required. We also consolidate mixed-brand orders, allowing you to procure these units alongside your regular deep-groove or spherical roller requirements in a single shipment. This eliminates the logistical friction of managing multiple international suppliers for your maintenance inventory, ensuring your critical spare parts arrive exactly when needed.
Documentation & Authenticity
Certificate of Conformity validating the specific contact angle suffix and polyamide cage material.
Original factory batch traceability linking the Gcr15 steel heat number to production records.
Running accuracy inspection reports confirming vibration grade V1, V2, or V3 compliance before dispatch.
Official brand QR verification codes printed on the packaging for immediate authenticity checks.
Dimensional inspection certificates verifying the exact bore and outside diameter tolerances.
Storage, Handling & Mounting
Keep the open seal units in their original vapor-corrosion inhibitor packaging until the exact moment of spindle assembly.
Use clean, lint-free gloves when handling the polyamide cage to prevent skin oils from degrading the polymer.
Induction heating is recommended for mounting the inner ring on the spindle shaft to preserve the selected clearance class.
Store the Gcr15 steel components in a climate-controlled environment to prevent microscopic rust on the open raceways.
Verify the contact angle marking on the outer ring before pressing to ensure the correct thrust load orientation.
Preparing Your Spindle Parameters for Technical Review
To ensure the selected contact angle and clearance class match your specific machining duties, please share the spindle’s maximum RPM, operating temperature range, and typical axial cutting forces. Providing the original equipment manufacturer’s part number allows our engineers to perform a precise cross-reference check against equivalent premium models. This technical review guarantees the replacement unit integrates flawlessly into your existing high-speed machinery, preventing unexpected vibration issues and extending the overall service interval of the spindle assembly.
Frequently Asked Questions
Q: How to verify the authenticity of S Kf bearings through official traceability channels?
A: You can scan the QR code on the packaging using the manufacturer’s official mobile application to confirm the origin. Additionally, request the original factory batch traceability documentation, which links the specific heat number of the Gcr15 steel to the production date and dimensional inspection records, ensuring the unit is not a counterfeit.
Q: What are the operational differences between 15°, 25°, and 40° contact angles for angular contact ball bearings?
A: A 15° contact angle provides the highest speed capability and radial rigidity, making it ideal for high-RPM spindles. A 25° angle offers a balanced compromise between speed and axial load capacity. The 40° angle maximizes thrust load support for heavy axial cutting forces but operates at lower maximum speeds due to increased sliding friction.
Q: How to select the correct clearance class for high-speed machine tool spindles?
A: High-speed spindles generate significant friction heat, causing the inner ring to expand more than the outer ring. Engineers typically select a larger internal clearance, such as C3 or C4, to compensate for this thermal expansion and the tight interference fit on the shaft. This prevents the bearing from seizing under operating temperatures.
Q: Why choose a nylon polyamide cage over a brass cage for high-speed pump applications?
A: Polyamide cages are noticeably lighter than brass alternatives, which reduces centrifugal forces on the rolling elements at high rotational speeds. The polymer material also provides excellent sliding properties and dampens high-frequency vibrations, resulting in quieter operation and lower friction heat generation, which is critical for maintaining fluid film stability in high-speed pumps.
Q: What are the cross-reference equivalents for this model in other premium brands?
A: This specific angular contact design can be cross-referenced to equivalent models from other premium manufacturers such as FAG, NSK, or NTN. When substituting brands, it is crucial to verify that the contact angle suffix, cage material, and precision class match exactly to ensure the replacement unit maintains the original spindle dynamics.
Shipping Information
EU Warehouse
3-7 working days (bonded stock)
Direct from China
Shanghai & Ningbo hubs (bulk / FCL)
Markets Served
DE · IT · PL · ES · NL · FR · EU+
Incoterms
DDP / DAP available on request
Minimum Order
Contact us for MOQ details
Documents Included with Every Shipment
EN and ISO Quality Certificates
Batch traceability and manufacturing standard
Material & Heat-Treatment Reports
Full material composition and process records
CE Declaration of Conformity
For bearing units and motion products
RoHS Compliance Declaration
Restriction of hazardous substances
EUR.1 Movement Certificate
Preferential origin for EU customs
Certificate of Origin
Country of manufacture documentation
Correct HS Codes
Pre-classified for smooth customs clearance
Commercial Invoice & Packing List
VAT-compliant intra-EU invoicing
Transparent Landed Cost with Tax Explanation
SKFEU provides full price transparency so EU buyers know exactly what they pay. No hidden duties, no surprise charges at customs.
VAT-Compliant Invoicing
All intra-EU transactions are invoiced with correct VAT treatment. B2B buyers with valid EU VAT numbers receive zero-rated invoices where applicable.
No Unexpected Import Duties
Goods shipped from our EU bonded warehouse arrive as intra-EU movements -- no import duties, no customs delays for EU-based buyers.
EUR.1 & Origin Docs Ready
For shipments direct from China, EUR.1 movement certificates and certificates of origin are prepared in advance to minimise customs clearance time.
DDP Pricing Available
Ask for Delivered Duty Paid quotations -- we absorb all import costs so your landed cost is fixed and predictable from day one.
Need a landed cost breakdown? Contact Sofia at
sofia@skfeu.com
or via WhatsApp for a full DDP quotation including freight, duties and VAT for your country.
Send Inquiry
Request Pricing & Availability
Share your requirements and Sofia will respond within one working day with pricing, lead time and full documentation details.